Why Your Bubble Wrap Machine Winds Uneven Rolls & How to Fix Clutch Slipping in the UAE
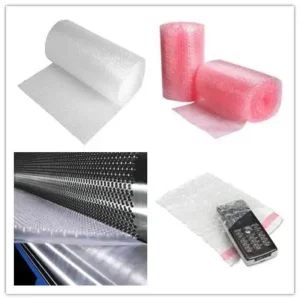
If you manage a protective packaging facility in Al Quoz, Sajaa Industrial Area, or Mussafah, you know that producing good air cushions is only half the job — how the roll looks when it ships decides whether the client accepts it or sends it back. A common problem in the Gulf region is the winding section losing control: telescoped roll ends, loose rewinding, and a slipping magnetic powder clutch.
Instead of crisp, even industrial rolls, the operator is left fighting ragged edges that look unprofessional. Many technicians first blame the operator or film thickness variation, but in Middle East conditions the real cause usually sits in the web tension control and thermal overload of the coupling. This guide explains why the machine fails to wind straight and the steps your engineering team can take to fix the clutch slipping.
The Middle East Environment VS Your Winding Tension Control
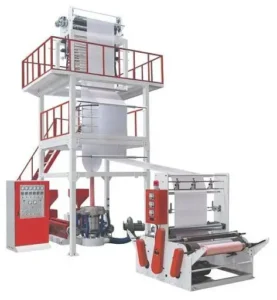
The line relies on precise taper tension control to move the film from the high-speed forming roller onto the finishing air shaft. As the roll diameter grows, the torque requirement rises with it, putting steady load on the magnetic powder or electromagnetic clutch.
In the UAE, that tension balance faces two environmental pressures: extreme factory heat and fine desert dust. When the warehouse temperature passes 40°C, the inside of a standard magnetic clutch can climb past 80°C. That heat makes the magnetic iron powder agglomerate, lose its fluid friction, and eventually bake into clumps — the result is clutch slipping and a sudden drop in transmission torque.
Sand in the air also slips past standard sealing rings and gets into the air gap between the rotor and stator. The abrasive dust creates uneven friction, and the web tracking drifts sideways during high-speed winding, which shows up as badly telescoped roll ends.
Step-by-Step Technical Fixes to Restore Winding Profile
Getting the rolls straight and the clutch gripping comes down to three jobs: overhaul the clutch, reset the taper tension, and check the lay-on roller.
First, deep-flush and replace the powder on the slipping clutch. Stop the machine and lock out the main circuit breaker. Let the clutch cool to a safe handling temperature and wear heat-resistant gloves before disassembling the housing — it runs hot and can burn. Use a clean brush and dry compressed air to clear trapped desert dust and contaminated metal fragments. Inspect the magnetic powder; if it looks dark brown, clumpy, or burnt, replace it with a good high-temperature spherical iron powder. That restores smooth electromagnetic shear and the winding shaft grips the core with steady torque.
Second, recalibrate the taper tension curve on the PLC. Running on constant tension builds up internal pressure, squeezing the inner layers outward and telescoping the roll. Rewrite the program to a declining taper profile that reduces the clutch output current by 30–40% as the roll nears its target diameter — a firm core with a slightly relaxed outer layer keeps the film from sliding out of alignment.
Finally, check the parallelism of the pneumatic lay-on roller and air entrapment. If the contact roller is even a millimeter off line with the winding air shaft, it pushes the film to one side continuously. Use a dial gauge to align the shafts and set the pneumatic regulators for uniform pressure across the web width, which squeezes out the boundary air that makes rolls loose and spongy.
Secure Clean Rolls and Maximize Factory Output
Keeping rolls straight and winding tight takes constant attention to the machine’s cooling and dust filtration. With the clutch protected from overheating and the taper tension dialed in, your plant can deliver clean, even rolls that meet the standards of the UAE logistics and e-commerce markets.
If your plant is dealing with persistent winding issues, or you are looking to replace older winding stations with a heavy-duty, multi-layer line — independent dual-shaft automatic cutting, dual-servo tension, and clutches built to run cool in tropical heat — our technical support engineers would be glad to review your setup.