UAE Plastic Extrusion Guide: How to Fix Blown Film Machine Gauge Variation
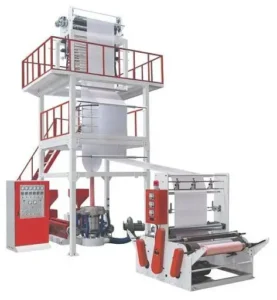
Operating a high-performance blown film machine in the UAE or Gulf region requires absolute precision, especially when summer temperatures in Dubai or Sharjah put extra stress on your cooling systems. Among all extrusion issues, film thickness instability—commonly known as gauge variation—is the most costly problem for Middle Eastern factories. When your film has thin or thick spots, it causes winding defects, wrinkles, and massive failures during downstream bag making or printing. To help you eliminate this waste, let us look directly at how to fix gauge variation by adjusting your air ring and die gap step-by-step.
Step-by-Step Guide: How to Fix Air Ring and Die Gap Issues Instantly
To fix gauge variation caused by uneven air ring airflow on your blown film machine, your very first action must be a thorough mechanical cleaning. You can fix localized thin spots by splitting the air ring and removing any polymer buildup, wax, or factory dust that has accumulated inside the lips, as even a microscopic blockage restricts cooling air and creates a hot, thin streak in the film. Next, ensure that the air ring is perfectly centered relative to the die cylinder using a dial indicator or precision centering gauge, because any off-center placement creates uneven air velocity around the bubble, leading to severe thickness deviations on your blown film extrusion machine.
To fix gauge variation originating from die gap misalignment, you must perform a precise manual or automatic bolt adjustment while the line is at operating temperature. You can fix a persistent thick spot in a specific sector by adjusting the die adjustment bolts located around the die head circumference, turning them carefully to close the die gap slightly in that exact zone. Always make these adjustments in small increments, such as a quarter turn at a time, and allow the bubble to stabilize for five to ten minutes before taking a new micrometer sample, ensuring the melt flow distributes evenly across the die lips of your co-extrusion blown film machine.
To fix severe gauge variation caused by ambient temperature interference, you must isolate the cooling zone from the surrounding factory climate. Fix this immediately by installing heavy-duty aluminum partitions or specialized physical wind shields around the lower tower section to block cross-drafts from open warehouse doors or local AC vents. Additionally, lock your chiller water temperature to a fixed setting and inspect your blower motor voltage, because any fluctuation in cooling air temperature or volume will instantly cause the frost line to wander, ruining the gauge uniformity on your blown film extrusion machine.
Process Troubleshooting Matrix for Film Gauge Variation
Use this quick-action reference guide to apply direct mechanical and process remedies to your factory floor.
| Blown Film Machine Gauge Defect |
Direct Fixes & Process Remedies |
Immediate Operational Action |
| Localized Thin or Thick Streaks |
Clean the air ring lips completely and remove all polymer or dust blockages. |
Disassemble the air ring lip, purge debris, and realign the airflow path. |
| One-Sided Gauge Variation |
Center the air ring precisely relative to the die and eliminate all mechanical tilt. |
Use a dial indicator to calibrate the air ring concentricity with the die lip. |
| Circumferential Thickness Errors |
Adjust the die gap bolts in small increments at the hot or thick spot sectors. |
Tighten or loosen the die adjustment bolts using a systematic micrometer check. |
| Random, Wandering Gauge Shifts |
Block all factory cross-drafts and lock the chiller cooling air temperature. |
Install physical tower wind shields and check blower motor speed stability. |
Pro-Tips for Maintaining Perfect Film Thickness
To ensure long-term gauge consistency on your blown film extrusion machine, implement a strict weekly maintenance routine for your die head and air ring assemblies. Clean condenser coils and check chiller fluid levels every single week without exception, because a minor efficiency drop in your cooling system will destroy your frost line control.
You can also eliminate manual adjustment errors completely by upgrading from basic manual die heads to an automatic gauge control system featuring a segmented air ring or thermal bolts. This technology upgrade monitors film thickness in real-time and adjusts the cooling profile automatically, locking in perfect tolerances on your co-extrusion blown film machine despite any shifting ambient factory temperatures.
Upgrade Your Factory with a Precision Blown Film Machine
We engineer every single blown film machine specifically to handle extreme tropical and desert operating environments without sacrificing micron-level precision. Our advanced air ring aerodynamics, integrated high-capacity chilling setups, and rigid heavy-duty tower structures ensure that your blown film extrusion machine stays rock-solid, delivering uniform film thickness even when the outside temperature hits 50°C.
If you want to eliminate gauge variations, lower your scrap rate, and invest in a reliable co-extrusion blown film machine built for the Middle East market, please contact our technical engineering team today for a custom machinery consultation.